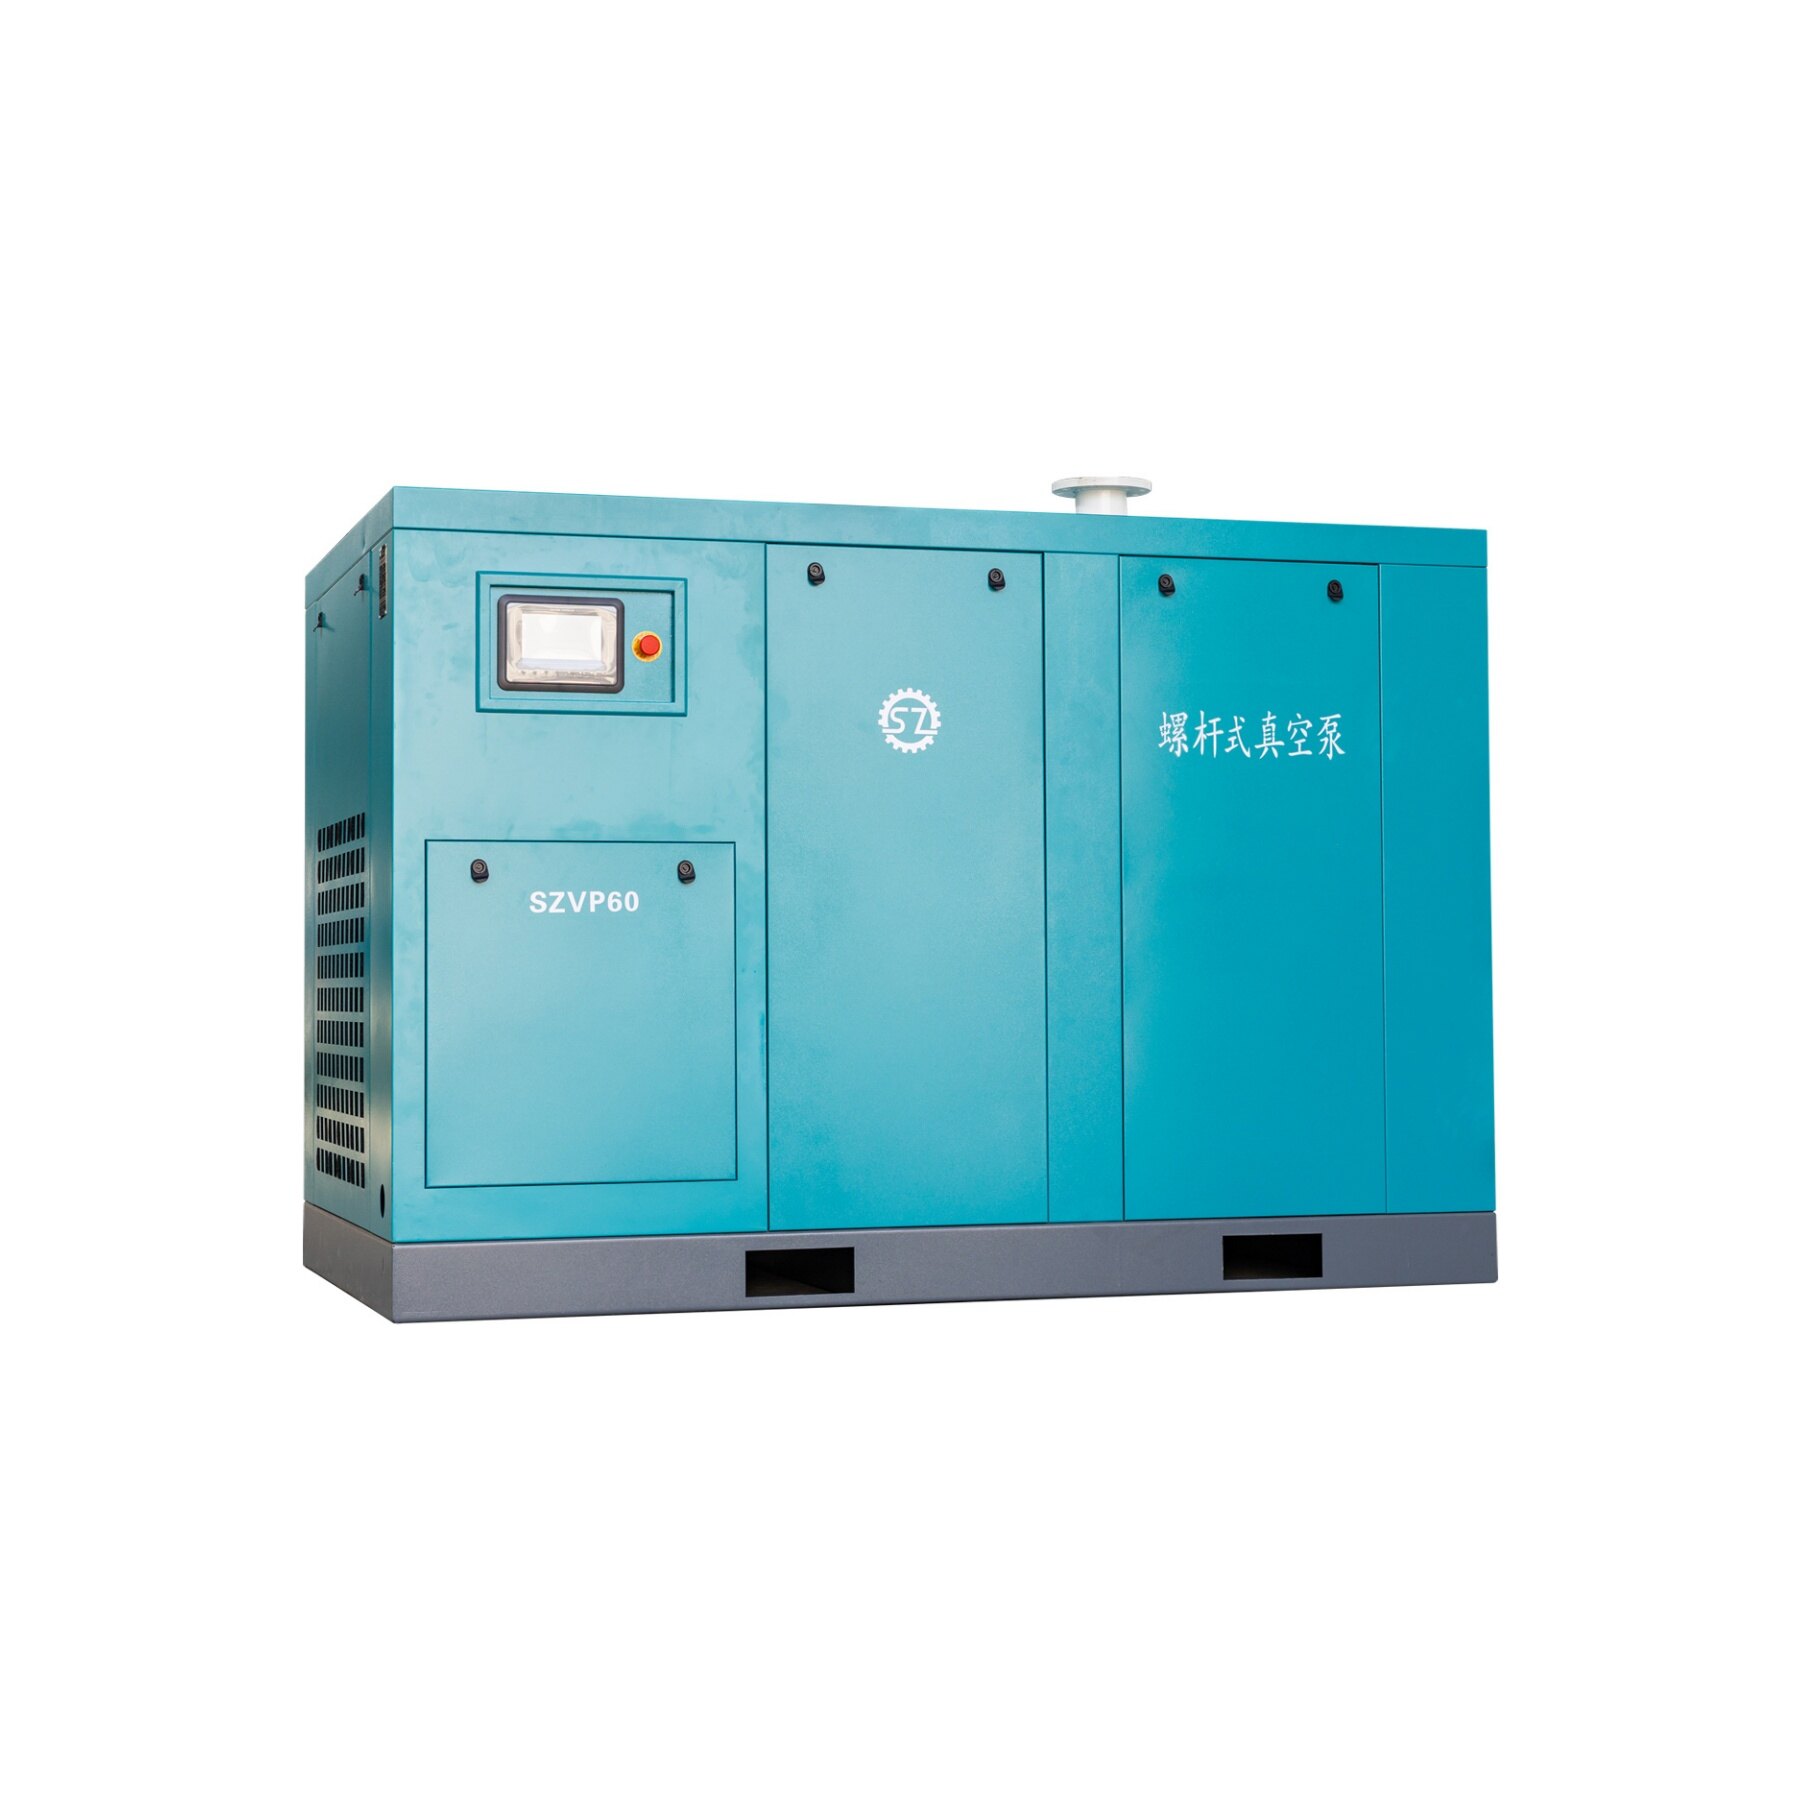
Sanzhi Permanent Magnet Variable Frequency Low-Oil Screw Vacuum Pump
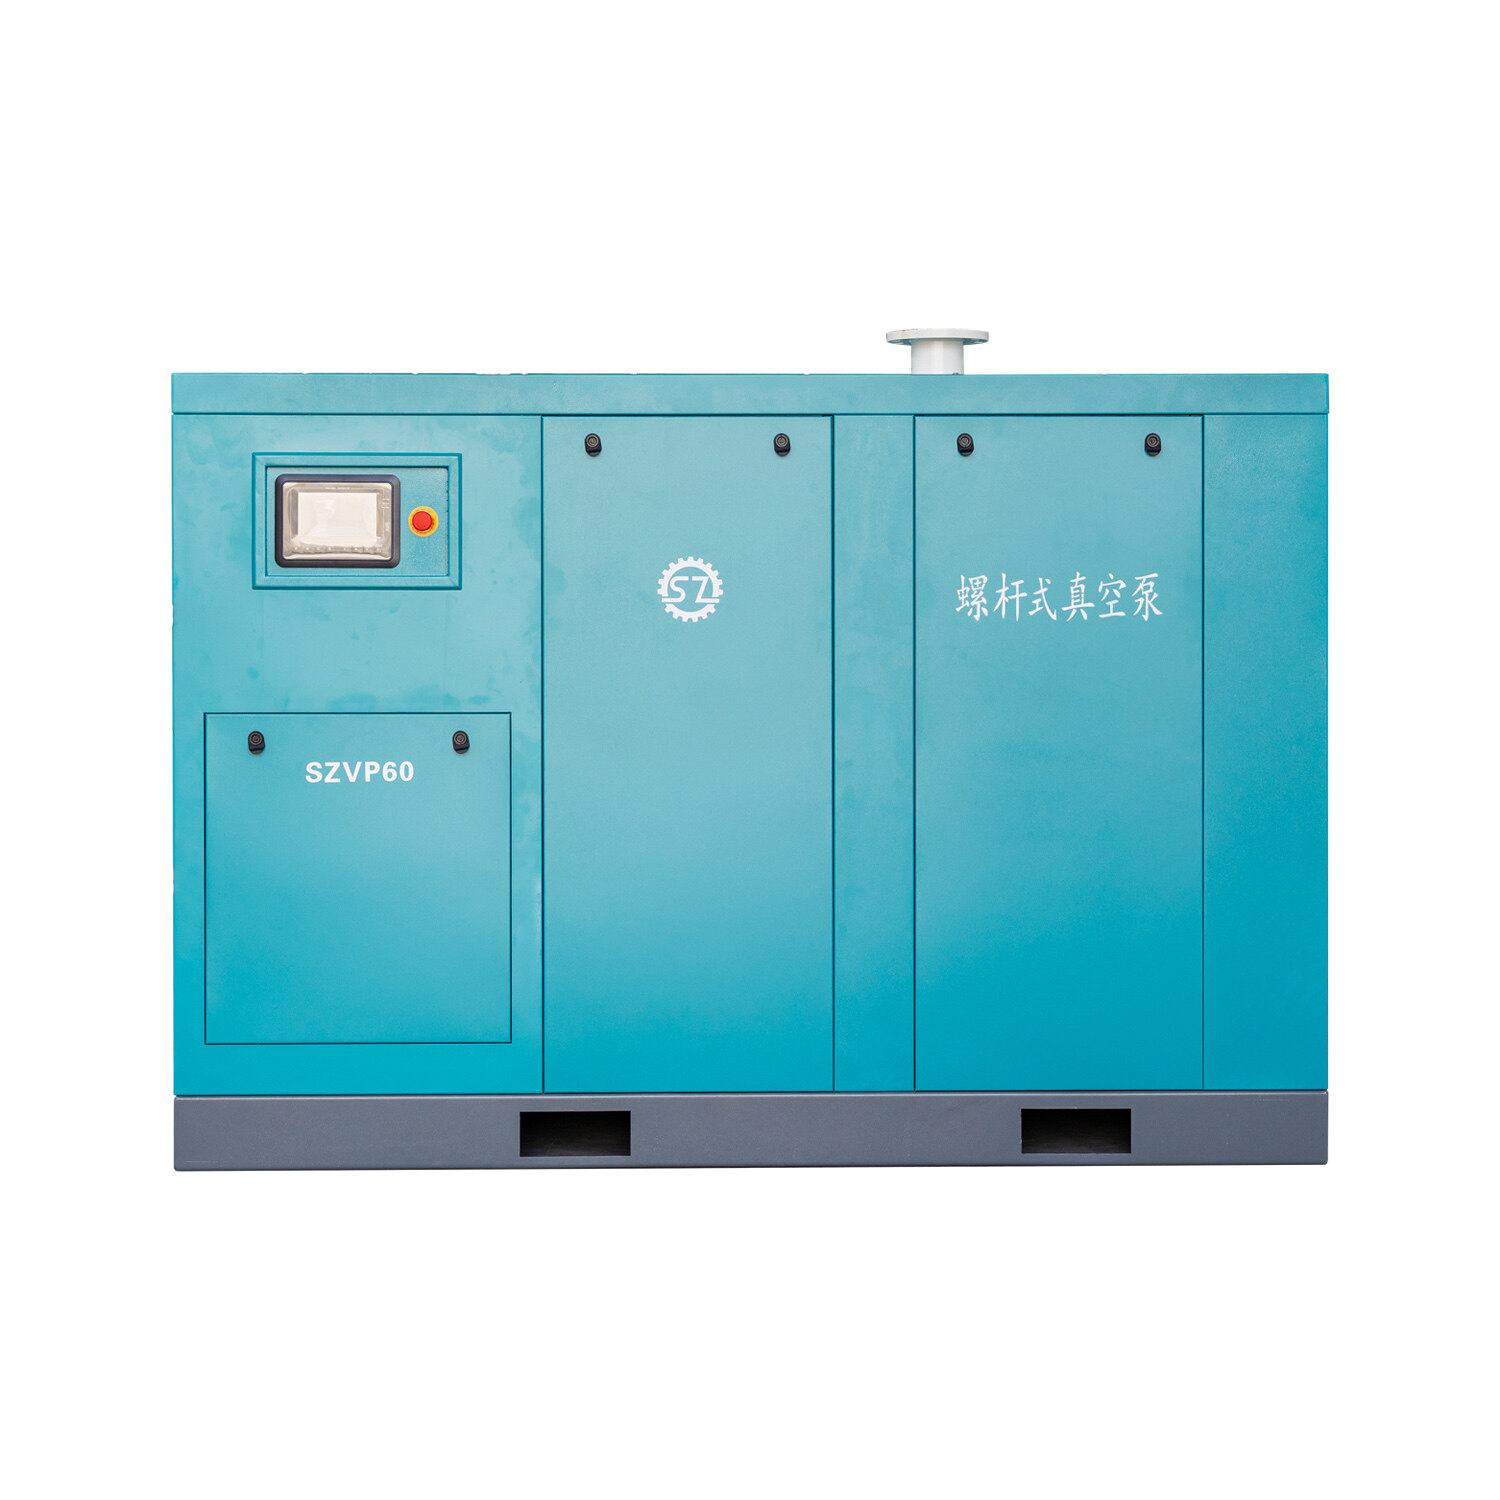
SZVP Micro-oil Permanent Magnet Variable Frequency Screw Vacuum Pump. Engineered for industrial negative pressure applications, achieving an ultimate vacuum of 0.098MPa (20mbar) and a working vacuum range of -0.05 to -0.098MPa. The permanent magnet variable frequency drive adjusts pumping speed on demand, delivering significant energy savings compared to traditional vacuum pumps. The micro-oil screw pump head ensures stable operation and can withstand minor moisture and dust. Its air-cooled design eliminates the need for cooling water and wastewater discharge, enabling easy installation. An intelligent touch-control system features built-in fault alerts and protection, supporting continuous long-term operation. It effectively replaces water ring and vane pumps, making it ideal for central vacuum stations, adsorption, dehydration, and degassing processes. Widely used in building materials, rubber & plastics, CNC machining, semiconductors, and solar PV processing industries.
Product Details
Sanzhi Micro-Oil Permanent Magnet Variable Frequency Screw Vacuum Pump
Product Overview
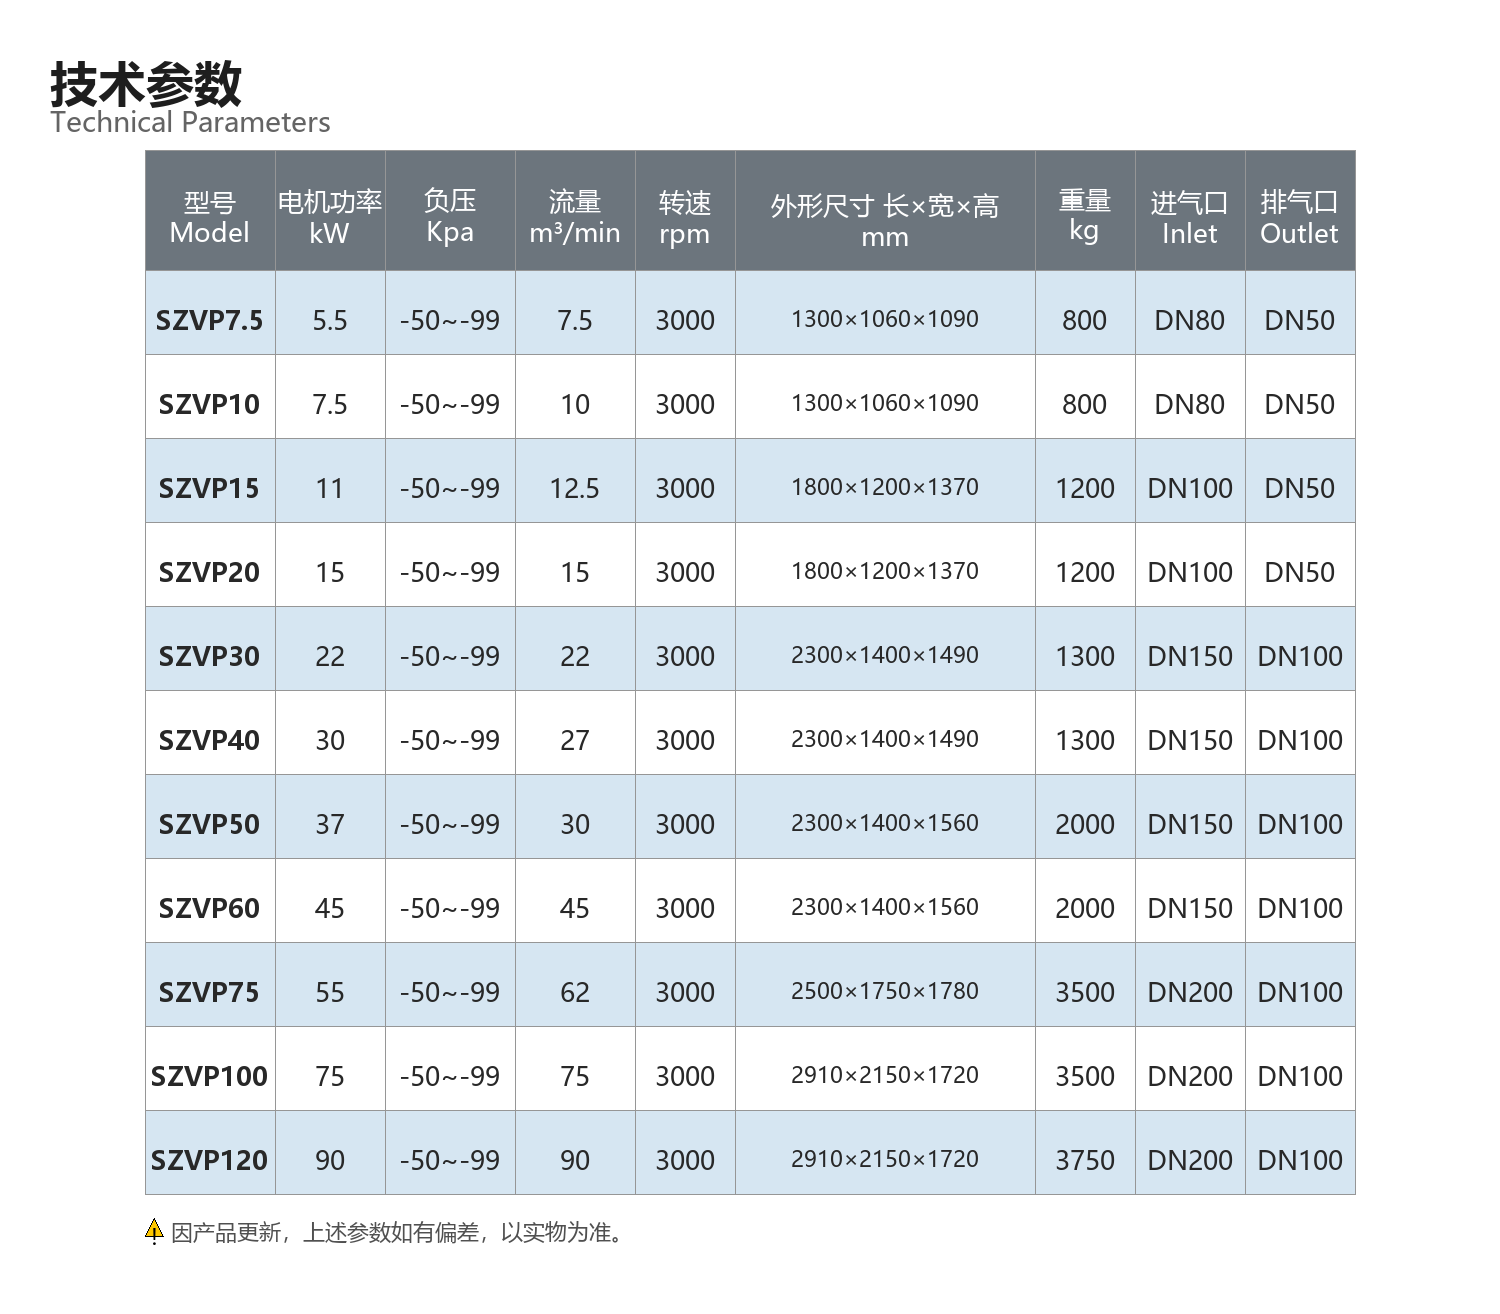
The SZVP series micro-oil permanent magnet variable frequency screw vacuum pump features a dedicated screw vacuum compressor, a micro-lubrication sealing structure, and an efficient permanent magnet variable frequency drive system. Operating gauge pressure: 0.05 to 0.098MPa.Maximum vacuum: -0.098MPa (absolute pressure 2 kPa / 2 mbar)Integrated all-in-one cabinet design replaces traditional water-ring and rotary vane vacuum pumps. Eliminates the need for cooling water, solving high energy consumption, excessive wastewater, and unstable vacuum issues common in conventional systems. Delivers stable industrial negative pressure air sources for factory central vacuum systems, process evacuation, and negative-pressure adsorption dehydration. Available in power ranges from 5.5 to 90 kW with multiple flow rate options to suit various continuous production scenarios.
Core Advantages
✅ Permanent magnet variable frequency drive for significant energy savings and reduced consumptionEquipped with a high-efficiency permanent magnet synchronous motor and an integrated variable frequency drive control system, it automatically adjusts speed based on actual on-site air demand to maintain constant vacuum pressure. Compared to traditional fixed-frequency vacuum pumps, it achieves comprehensive energy savings of 25‑60%, eliminates no-load energy consumption, and reduces long-term electricity costs for enterprises. Variable frequency start-up minimizes grid impact, making it ideal for 24-hour continuous operation.
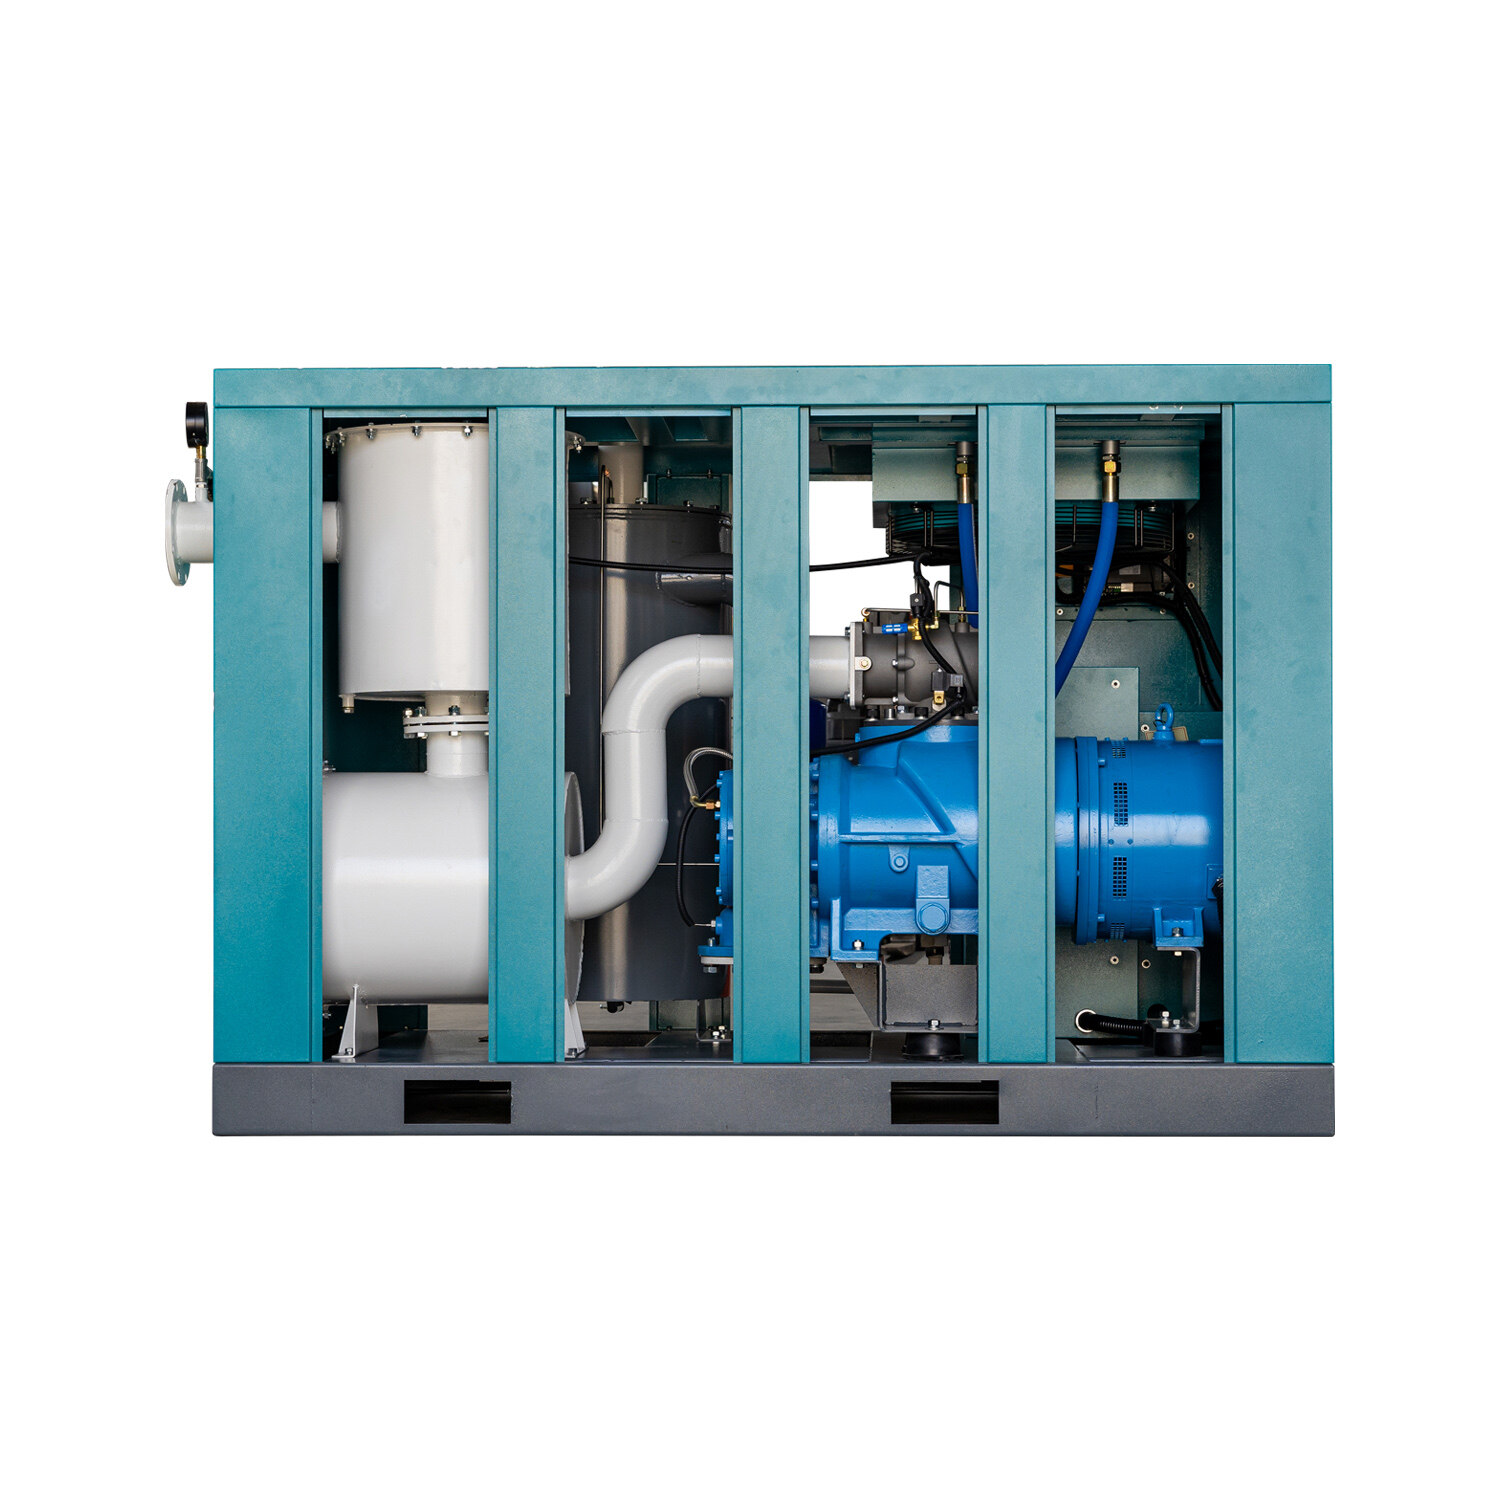
✅ Oil-injected screw compressor, stable and reliable vacuumVacuum-specific precision screw rotor with micro-oil lubrication and seal, ensuring non-contact friction for high volumetric efficiency. Achieves ultimate vacuum of 20mbar, operates stably in negative pressure range from ‑0.05 to ‑0.098MPa, resists minor water vapor and dust conditions without vacuum decay. Unlike water ring pumps, performance remains unaffected by water temperature, maintaining consistent vacuum levels without scaling or clogging issues.
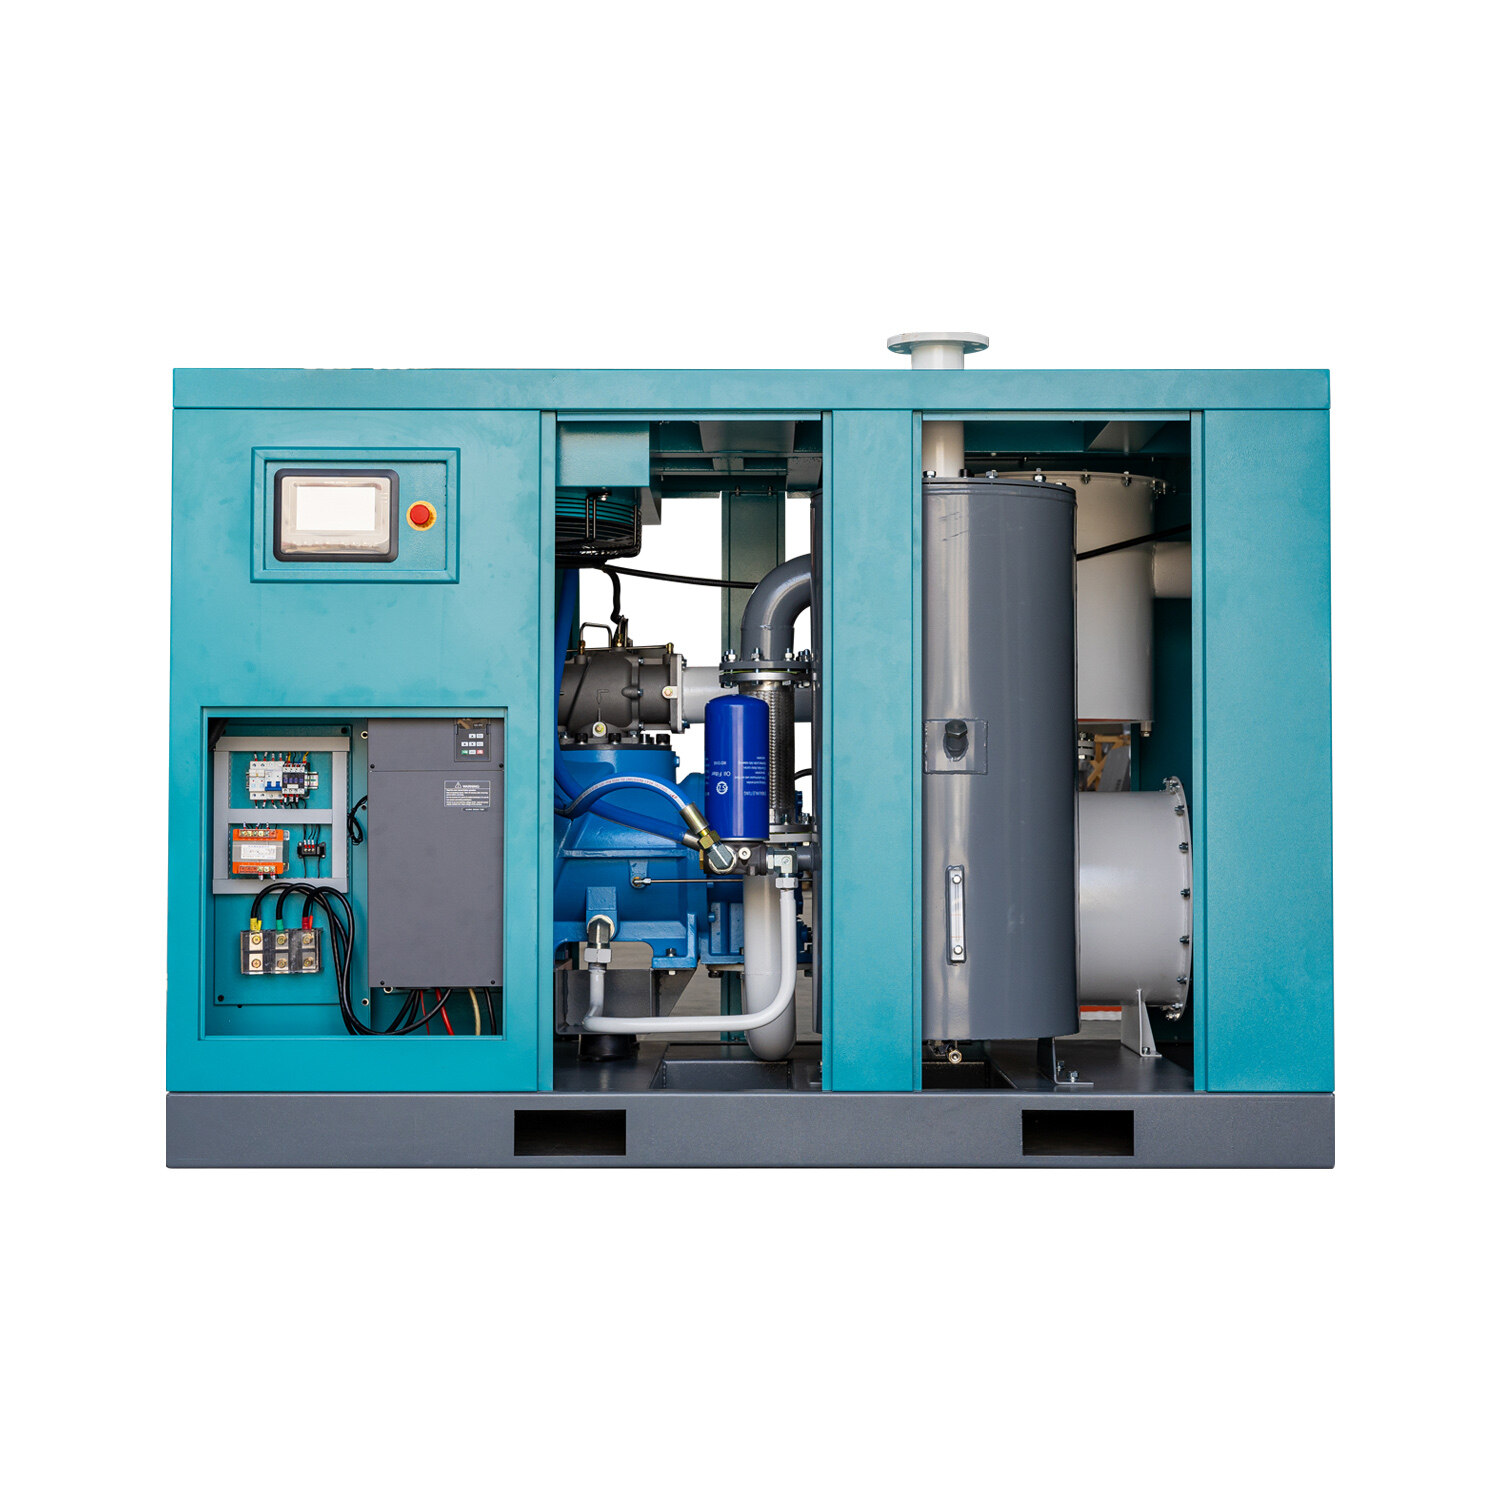
✅ Coolant-free design for easy installation and maintenanceComplete air-cooled integrated systemNo cooling water system required; no wastewater discharge.Eliminates the need for a sump and circulation pump, reducing initial investment. The all-in-one cabinet design features a compact footprint—simply connect to power and vacuum lines to start production. Its large-opening maintenance structure allows easy access for filter, oil-gas separator, and lubricating oil replacement, simplifying upkeep and minimizing downtime.
✅ Smart Touch Control SystemHigh-definition color touch display with real-time monitoring of vacuum pressure, operating current, temperature, and runtime. Features built-in fault alarms, maintenance reminders, and safety shutdown protection; supports operation data logging. Expandable IoT remote monitoring for anytime access to device status, reducing on-site management complexity.
✅ Low-noise protective chassis, workshop-friendlyInternal multi-layer noise reduction and vibration damping structure for low operating noise. Sealed sheet metal enclosure provides dust protection and splash resistance, ideal for indoor factory installation to improve workshop working conditions.
Use Cases
Widely used for negative pressure vacuum extraction and adsorption processes in industries such as factory central vacuum systems, CNC suction, vacuum dewatering, material degassing, thermoforming, ceramics and tiles, packaging, chemical processing, construction materials, printing, rubber and plastics. Supports both standalone batch operation and centralized vacuum station deployment.
Technical Notes
Working pressure range: 0.05 to 0.098MPa; Ultimate vacuum (gauge): 0.098MPa (absolute pressure 2 kPa, 20mbar); Actual vacuum may vary due to site leakage, altitude, and inlet medium conditions. Parameters are subject to product updates; refer to the actual equipment for specifications.